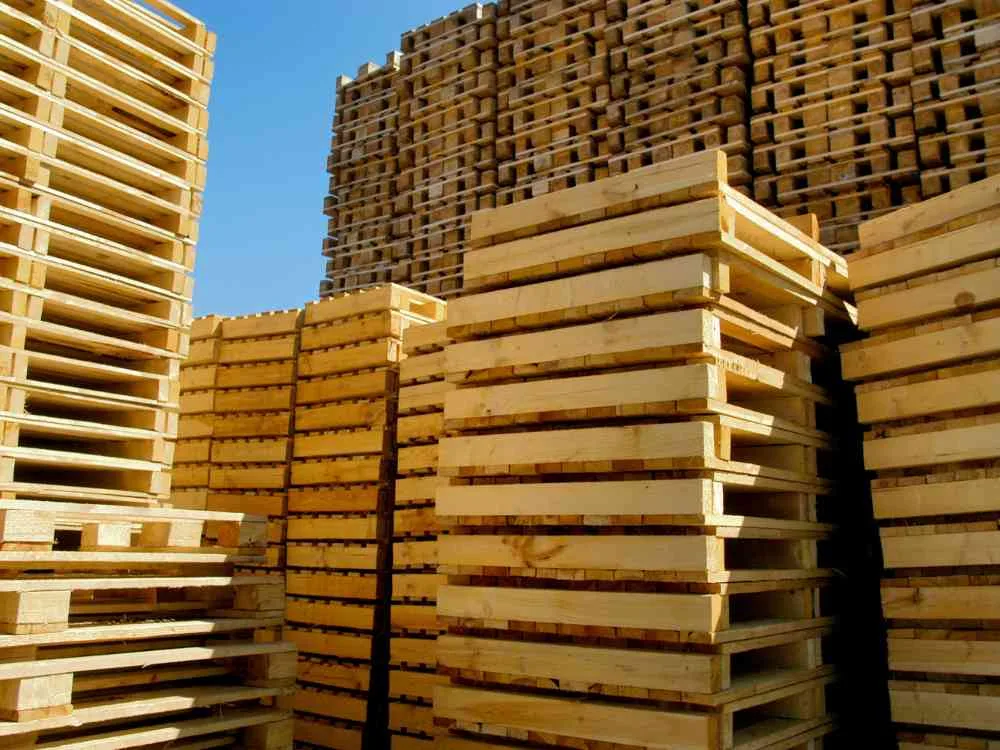
In the logistics and supply chain industry, pallets play a crucial role in the transportation and storage of goods. The evolution of pallet engineering has introduced various types of pallets, each with unique advantages. Among these, heat-treated GMA (Grocery Manufacturers Association) pallets have gained significant attention due to their durability and compliance with international regulations. Understanding the benefits of using heat-treated GMA pallets can be instrumental in optimizing supply chain operations and ensuring the safety and quality of transported goods.
Understanding Heat-Treated GMA Pallets
Heat-treated GMA pallets are designed to meet specific standards that enhance their usability and compliance. The heat treatment process involves subjecting the wooden pallets to high temperatures, which eradicates pests and pathogens, making them suitable for international shipping.
- Compliance with International Standards: By adhering to ISPM-15 (International Standards for Phytosanitary Measures No. 15), heat-treated pallets are accepted globally, facilitating smooth cross-border shipments.
- Enhanced Durability: The heat treatment process strengthens the wood, increasing the lifespan and resilience of the pallets under heavy loads.
- Environmental Sustainability: Heat treatment is a chemical-free process, making these pallets eco-friendly and safe for various industries.
This type of pallet is essential for businesses looking to streamline their supply chain logistics while maintaining high standards of safety and compliance. Discover expert strategies here.
Key Benefits of Heat-Treated GMA Pallets
Improved Load-Bearing Capacity
Heat-treated GMA pallets are known for their superior load-bearing capabilities. This is due to the structural integrity achieved through the heat treatment process. Businesses dealing with heavy or bulk goods can greatly benefit from the robustness of these pallets.
- Supports Heavier Loads: Suitable for industries like automotive and manufacturing where heavy loads are a norm.
- Reduces Risk of Breakage: Minimizes the possibility of pallet failure during transit, ensuring the safety of goods.
For businesses aiming to maximize efficiency in their logistics, learn about our tailored solutions.
Enhanced Safety and Hygiene
The heat treatment process eliminates pests, fungi, and other harmful microorganisms, making these pallets safer for handling food products and pharmaceuticals.
- Prevents Contamination: Ensures that goods remain uncontaminated during transportation.
- Complies with Sanitary Regulations: Meets the high sanitary standards required for shipping sensitive goods.
This aspect is crucial for industries where hygiene is a top priority. Find out more about this approach.
Economic and Operational Advantages
Aside from the logistical benefits, heat-treated GMA pallets offer significant economic advantages as well.
- Cost-Effective: Their durability and long lifespan reduce the need for frequent replacements, saving costs in the long run.
- Streamlined Operations: The standardized size and design of GMA pallets simplify handling and storage, enhancing operational efficiency.
For businesses looking to optimize their pallet usage, explore advanced guides and tips.
Conclusion
Incorporating heat-treated GMA pallets into the supply chain is a strategic move for businesses aiming to enhance efficiency, compliance, and safety in their operations. These pallets offer a blend of durability, environmental friendliness, and international compliance, making them a wise choice for various industries. Understanding these benefits allows businesses to make informed decisions that align with their operational goals and regulatory requirements.
For more insights and information on utilizing the best pallet strategies, explore advanced guides and tips to optimize your supply chain logistics.